Description
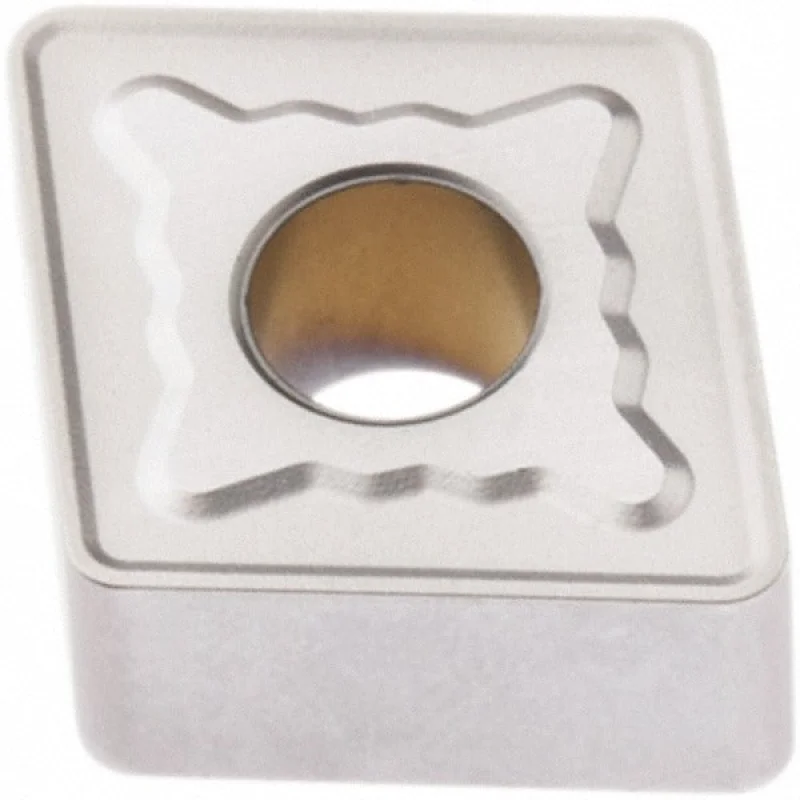
The SECO 02960451 is a CNMG432-MR7 series indexable turning insert manufactured from solid carbide with a CVD-applied Duratomic multilayer coating consisting of TiCN, Al2O3, and Cr. It carries the TP1501 manufacturer grade and is designed for negative-rake material removal in CNC turning, facing, and boring operations. The insert features an 80-degree diamond shape (shape code C), a 1/2-inch inscribed circle, a 0.0315-inch corner radius, and a T-Land cutting edge style with the MR7 chip breaker geometry. Four usable cutting edges are available per insert. Licensed HVAC technicians, machinists, and CNC operators handling steel and cast iron applications will find this insert suited for medium to semi-finish cutting conditions.
This insert is engineered primarily for steel workpiece materials (ISO material code P) at material grades P10 and P20, with secondary suitability for cast iron and hard materials (ISO codes K and H). Typical applications include external and internal turning, facing passes, and boring operations on CNC lathes and turning centers in both production-shop and job-shop environments. The MR7 chip breaker geometry is optimized to control chip flow during medium-depth cuts on ferrous materials. Maximum depth of cut reaches 0.4764 inches, making this insert appropriate for moderate stock removal as well as finishing passes.
Key Features
- Duratomic CVD multilayer coating (TiCN, Al2O3, Cr) for extended tool life on steel and cast iron
- TP1501 grade with MR7 chip breaker geometry for controlled chip evacuation in medium cutting conditions
- 80-degree diamond insert shape with T-Land cutting edge for improved edge strength
- Four cutting edges per insert for cost-effective indexing
- Compatible with clamp, pin, and lever-lock insert holding methods
- Multi-use geometry supports turning, facing, and boring in a single insert style
Compatibility
Designed as a direct replacement for toolholders and boring bars accepting CNMG432 (ISO: CNMG120408) style inserts with clamp, pin, or lever-lock clamping. Conforms to ANSI and ISO standards for CNMG-series inserts. Verify toolholder pocket geometry and insert seating before installation.
Installation Notes
Installation is performed by qualified machinists or CNC setup technicians. Ensure the machine spindle is fully stopped and locked out before indexing or replacing inserts. Use the appropriate torque wrench and clamping hardware specified by the toolholder manufacturer do not overtighten clamping screws, as this can fracture the carbide insert. Inspect the toolholder pocket for damage or debris before seating a new insert to ensure proper insert support and edge alignment.
Technical Specifications
- Insert Style: CNMG
- Industry Standard Number: CNMG432-MR7
- ISO Code: CNMG120408-MR7
- Manufacturer Grade: TP1501
- Chip Breaker: MR7
- Insert Shape: Diamond 80 (80-degree included angle)
- Insert Material: Solid Carbide
- Coating: TiCN, Al2O3, Cr (Duratomic CVD)
- Cutting Edge Style: T-Land
- Insert Hand: Neutral
- Rake: Negative
- Number of Cutting Edges: 4
- Inscribed Circle: 1/2 inch (0.5000 inches)
- Insert Length: 0.5079 inches
- Insert Thickness: 3/16 inch (0.1874 inches)
- Corner Radius: 1/32 inch (0.0315 inches)
- Hole Diameter: 0.2028 inches
- Maximum Depth of Cut: 0.4764 inches
- Clearance Code: N
- Tolerance Code: M
- Insert Holding Method: Clamp, Pin, Lever Lock
- Primary Workpiece Material: Steel (P10, P20)
- Secondary Workpiece Material: Cast Iron, Hard Material
- Coating Process: CVD
- Standards: ANSI, ISO
- Weight: 0.02 pounds
- Package Quantity: 1 insert per package (minimum order quantity: 10)
Standard Information
- Brand: SECO
- Manufacturer Part Number: 02960451